


Four properties hidden inside the word “finish”
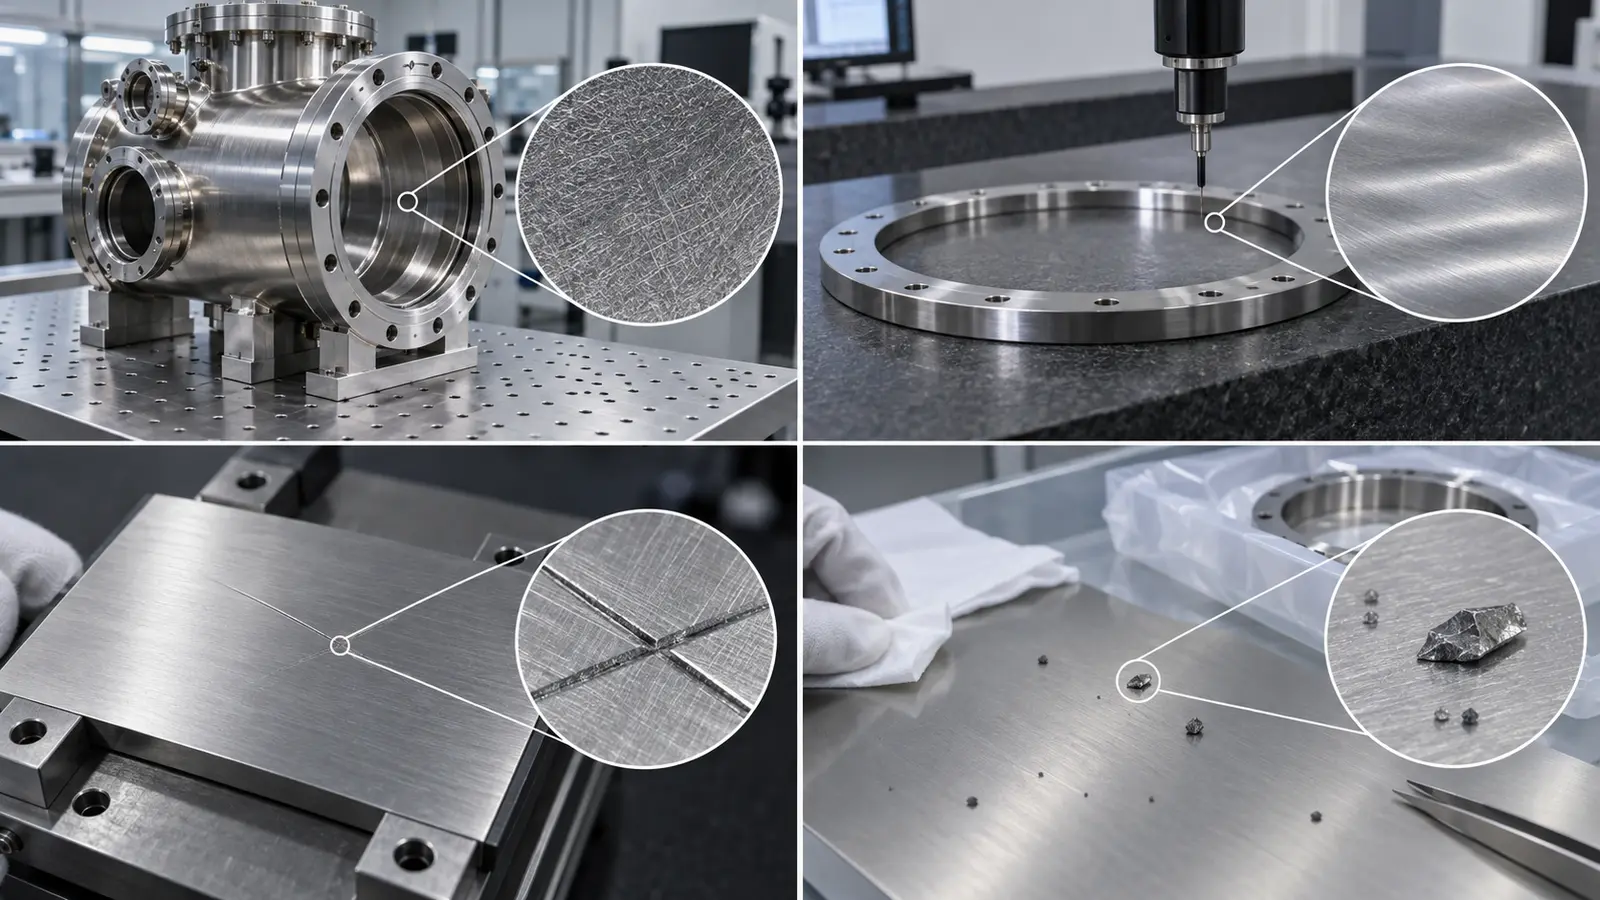
A procurement note that says “polished and clean” combines several independent requirements without defining any of them. Separate texture, geometric form, surface condition and residual contamination before selecting a finishing process.
| Proprietà | What it describes | Example of a separate requirement |
|---|---|---|
| Texture | Small-scale surface height variation | Specified roughness parameter, measurement direction and locations |
| Form | Overall shape of the functional surface | Seal-land flatness in a defined inspection condition |
| Surface condition | Local defects, burrs or treatment discontinuities | No unacceptable scratch crossing the seal contact path |
| Pulizia | Residual particles, films or chemical contaminants | An agreed cleaning and contamination-assessment procedure |
Ra is the arithmetic mean of the absolute profile deviations from a mean line over an evaluation length. It reduces a measured profile to one parameter; it does not identify the chemistry on the surface or guarantee the absence of a damaging scratch.
For semiconductor equipment, the process owner should define which contamination matters and how it will be assessed. A photograph of a shiny wall is not equivalent to a particle, residue or vacuum-performance test.
Divide the drawing into functional surface zones
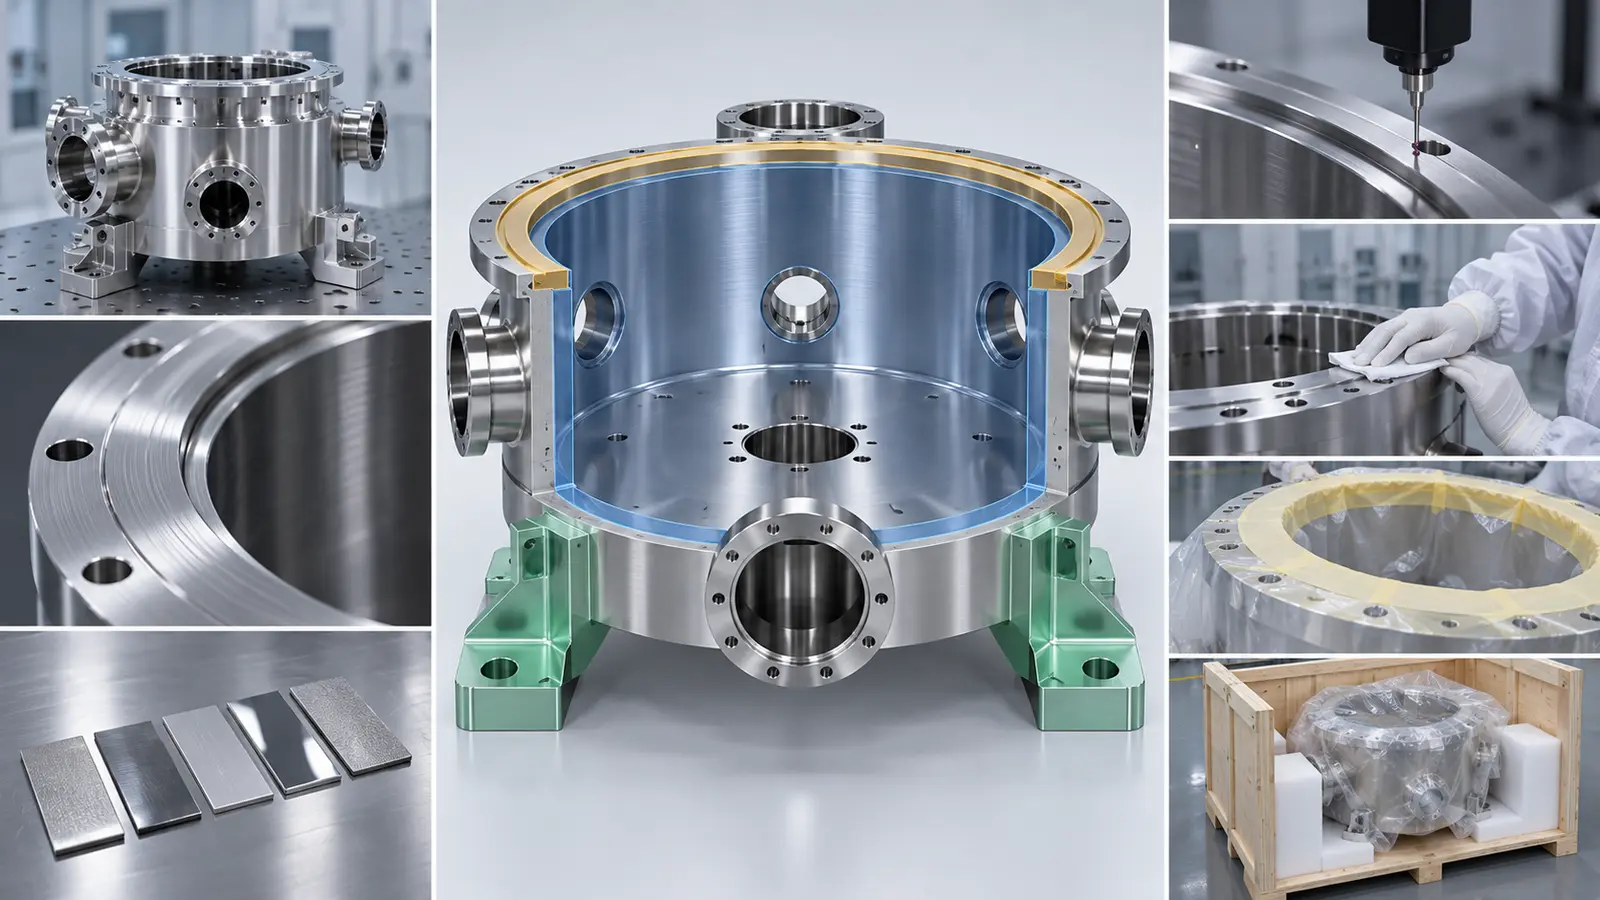
Different parts of a chamber deserve different instructions. Applying the most demanding finish everywhere increases cost and can damage features whose geometry matters more than appearance.
Seal lands and gasket interfaces
These surfaces must support the specified seal. Local scratches, tool marks, edge damage and waviness can matter alongside roughness. Preserve the dimensions and edges required by the sealing system; indiscriminate polishing can round a critical feature or change a gland’s effective height.
Process-facing walls and removable shields
The appropriate condition depends on exposure. A chamber wall, a plasma-facing liner and a deposition shield do not necessarily need the same texture. A shield may need a qualified surface that manages deposited-film adhesion; that is a different objective from minimizing roughness on a seal land.
External supports and mounting surfaces
These surfaces may require corrosion protection, assembly flatness or handling durability without sharing the vacuum-side cleanliness specification. Mark boundaries so a supplier does not apply an external cosmetic treatment to a process-facing region.
Use the same exposure-based logic described in semiconductor equipment material selection. The substrate and the final surface together determine compatibility; neither can be selected in isolation.
Select the process after defining the result
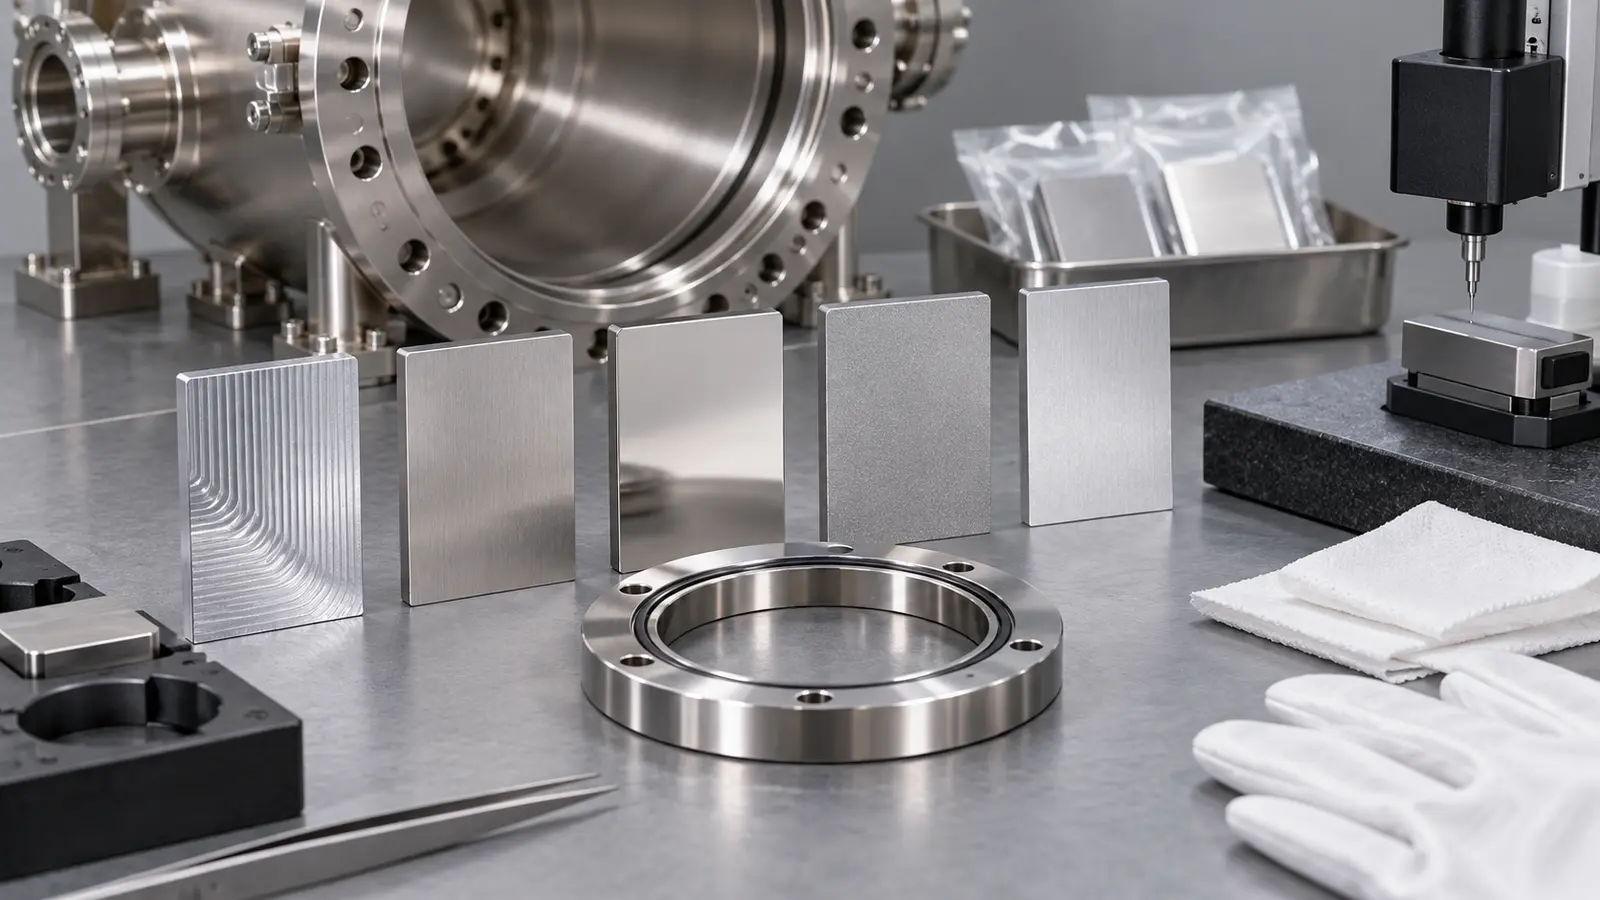
| Finishing route | Potential purpose | What still needs control |
|---|---|---|
| Controlled machining | Produce functional texture while preserving geometry | Tool condition, burrs, lay, fluid removal and local defects |
| Mechanical polishing | Modify texture on accessible surfaces | Material removal, edge rounding, embedded abrasive and cleaning |
| Electropolishing suitable stainless steel | Electrochemically remove surface material | Dimensional change, accessible geometry, chemistry and subsequent cleaning |
| Passivation of suitable stainless steel | Support corrosion resistance through an approved chemical treatment | Prior cleaning, alloy compatibility and verification requirements |
| Anodizing or other qualified coating | Provide specified surface behavior on the selected substrate | Thickness, porosity, masking, adhesion and process compatibility |
These processes are not synonyms. Passivation is not a dimensional smoothing operation equivalent to electropolishing. A coating cannot be specified solely by color. Mechanical polishing may improve an accessible surface while leaving a deep passage untouched.
When reviewing surface finishing options, include the actual geometry and intended exposure. A service’s availability does not by itself qualify that finish for semiconductor process contact.
The Kurt J. Lesker vacuum chamber technical notes discuss chamber construction and material considerations. Their broader lesson for a purchase specification is that the proposed surface must be compatible with the chamber’s material, construction and operating conditions—not merely attractive.
Sequence machining, treatment and cleaning deliberately
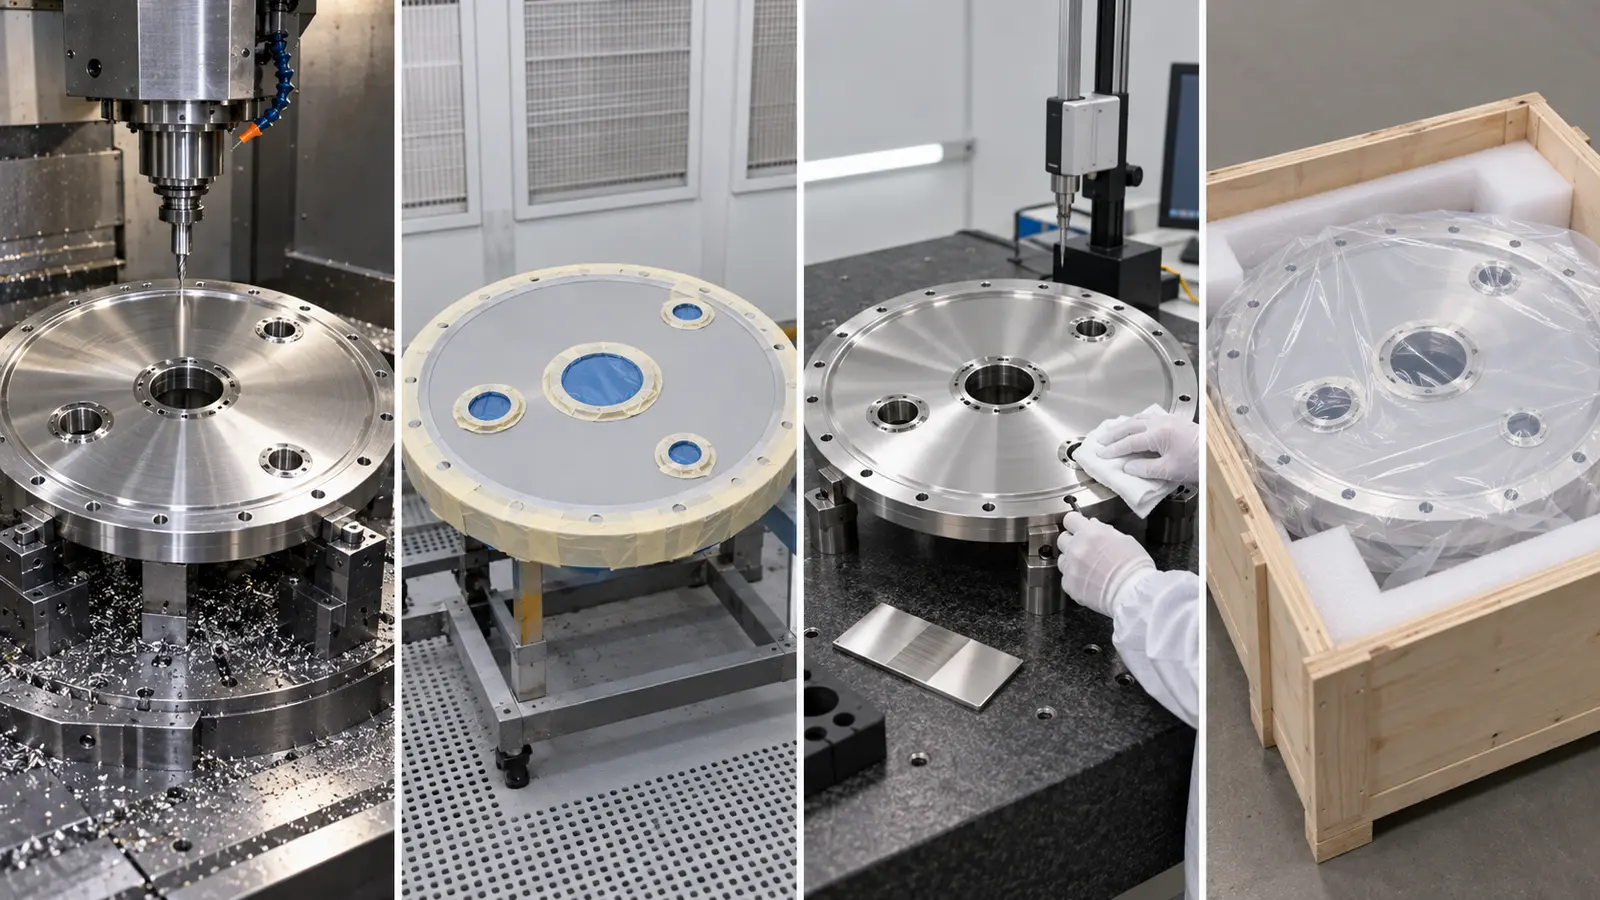
A dimensional report issued before a material-removing treatment may no longer describe the delivered part. A coating can also change clearance, thread fit and sealing geometry. The manufacturing route should state when each critical requirement becomes final.
- Establish the stock and datum plan. Identify which features control assembly and where finishing allowances are needed.
- Complete operations that create chips or distortion. Include relevant joining and any approved stabilization steps.
- Machine and inspect critical geometry at the specified stage. Make explicit which dimensions apply before or after treatment.
- Apply the approved finish with defined masking. Keep excluded sealing or grounding areas identifiable.
- Clean, inspect and protect the delivered condition. Avoid sending an accepted surface back into uncontrolled handling.
For a chamber with narrow ports, review fluid drainage, access and the ability to remove residues from internal intersections. A blind feature may pass visual inspection at its opening while retaining contamination deeper inside.
Il machining route for chamber bodies and lids should therefore be reviewed with finishing requirements before production starts. Leaving all surface decisions until after machining can make an otherwise acceptable component difficult to finish or inspect.
Packaging is part of this sequence. Protect sealing lands without introducing an unapproved adhesive, lint source or contact material. If a clean package must be opened for incoming inspection, define how the controlled condition will be restored.
Replace vague drawing notes with verifiable requirements
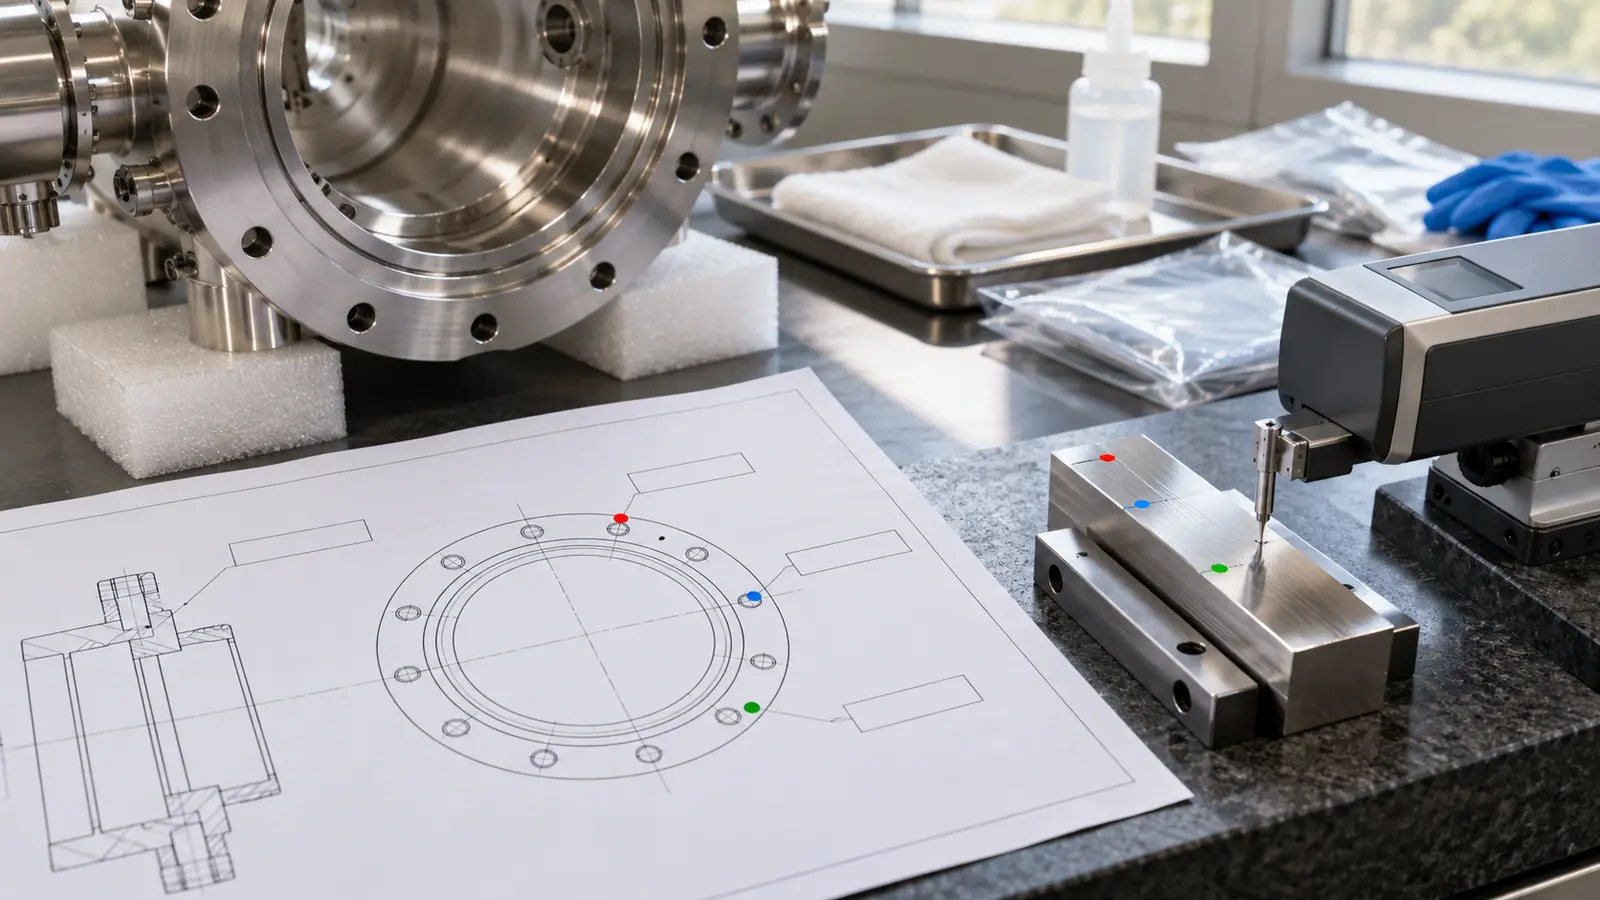
The following examples illustrate specification structure, not universal acceptance limits. The designer must supply the actual values and approved procedures for the equipment.
| Ambiguous note | More useful instruction |
|---|---|
| Mirror polish all surfaces | Identify the required texture by surface zone and preserve specified edges and dimensions |
| Vacuum clean | Reference the approved cleaning, drying, handling and assessment procedure |
| No scratches | Define functional defect criteria and inspection conditions for seal and process surfaces |
| Anodize | Identify the approved treatment, thickness range, masking and acceptance requirements |
| Inspect surface finish | State measurement parameter, locations, direction and the relevant measurement settings |
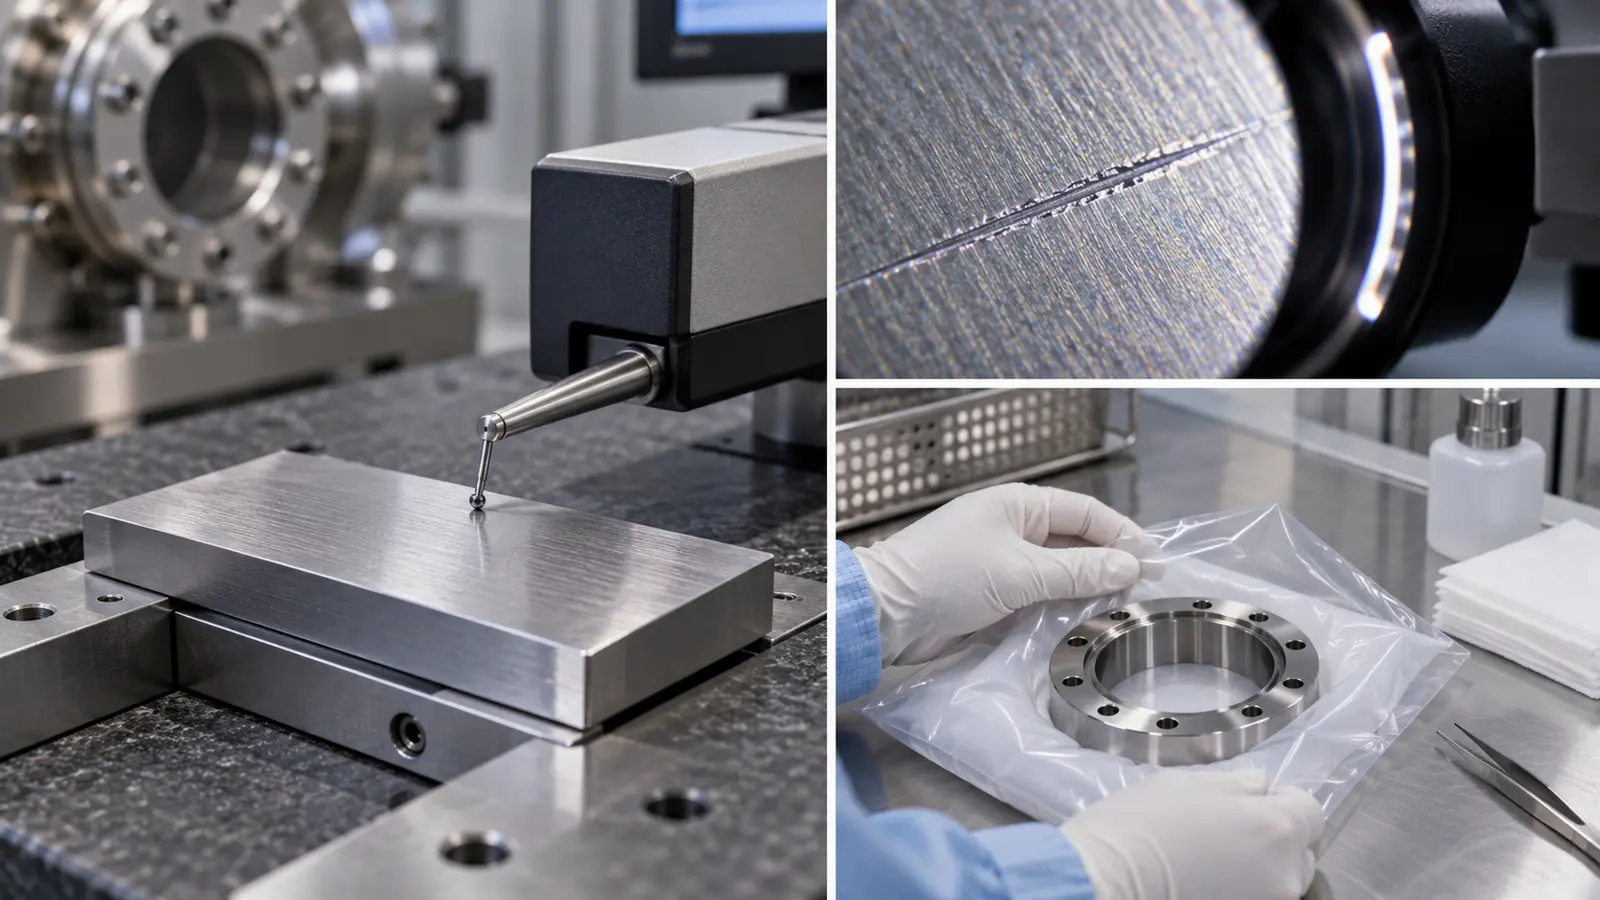
Choose a measurement method that can reach the surface being specified. A contact instrument that works on an open lid may not access a recessed internal wall. If a witness coupon is proposed, define what it represents and what it cannot prove about the actual part.
Keep changes traceable. Switching an abrasive, treatment supplier or cleaning procedure may affect the final surface even when the nominal drawing note remains unchanged. The required change-control level depends on the part’s role and customer specification.
Jucheng Precision can review the machining and finishing requirements for a custom component against the drawing. Include the surface-zone map and acceptance method in the request so the deliverable is an agreed condition, rather than an undefined promise of “semiconductor-grade” quality.
What a surface inspection can—and cannot—establish
Does a low Ra guarantee a leak-tight seal?
No. A low measured roughness does not establish flatness, correct seal compression or the absence of a local scratch. Inspect the whole functional interface and verify the assembled joint under the specified conditions.
Should every stainless chamber be electropolished?
No. The process must solve a defined requirement and suit the alloy, geometry and dimensional allowance. Some surfaces are better addressed by controlled machining and cleaning; others may justify an additional treatment.
Can surface appearance prove low outgassing?
No. Gas release depends on material, preparation, contamination and test conditions. A vacuum-performance requirement needs an appropriate assessment rather than inference from reflectivity.
The release decision: accept a chamber surface against its functional requirements. Texture measurements, dimensional inspection, contamination assessment and leak testing provide different evidence. Keeping them separate makes failures easier to diagnose and supplier quotations easier to compare.

