


Una filettatura è essenzialmente un cuneo avvolto attorno a un cilindro. È l'interfaccia meccanica più comune nell'hardware moderno, eppure rimane la caratteristica più fraintesa sul letto della macchina CNC. Ogni anno, migliaia di componenti costosi raggiungono la fase finale di linee guida di progettazione per la lavorazione CNC implementazione, solo per essere rottamati perché un maschio si è rotto all'interno di un foro cieco. Questo non è solo un incidente di officina; di solito è un fallimento progettuale nato dalla mancanza di rispetto per le dinamiche dell'utensile. Una Guida alla Progettazione di Filettature CNC non riguarda la scelta di una dimensione del bullone, ma la gestione della coppia, dell'evacuazione del truciolo e dell'elasticità del materiale.
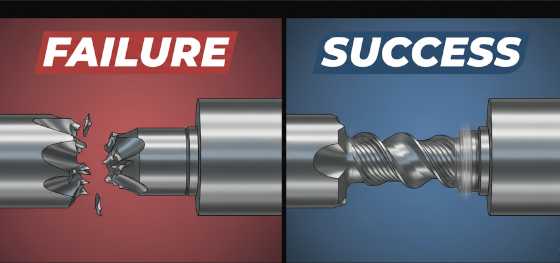
Il team di ingegneria di JUCHENG ha eseguito migliaia di audit DFM in cui parti "sovra-filettate" hanno creato rischi di produzione inutili. Abbiamo visto progetti che specificano filettature M3 fino a una profondità di 20 mm in titanio di grado 5, una richiesta geometrica che sfida i limiti fisici degli utensili in carburo. Se il tuo progetto tratta un foro filettato come un semplice cilindro 3D con una texture, stai invitando ritardi di produzione. Questa guida va oltre le tabelle standard per esplorare la meccanica effettiva dell'ingaggio della filettatura e come JUCHENG utilizza tecniche avanzate di fresatura e formatura per garantire che i tuoi assemblaggi siano robusti e il tuo progetto rimanga nei limiti del budget.
Il costo reale di una filettatura non è il tempo necessario per tagliarla; è il rischio che comporta per il pezzo. Quando progetti una filettatura, stai progettando un punto di rottura per l'utensile. Analizziamo le leggi fisiche della profondità della filettatura, della preparazione del foro e della selezione dell'utensile che definiscono un modello CAD pronto per la produzione.
La Trappola della Profondità: Fisica della Regola del 3x Diametro
Interno vs. Esterno: Gestione di Classi di Accoppiamento e Tolleranze
L'Equazione del Foro per Maschio: Logica della Percentuale di Filettatura
Fresatura di Filettature: Lo Scudo Strategico per Leghe di Alto Valore
Standard di Affidabilità di JUCHENG: Pianificazione del Processo per Filettature
La Trappola della Profondità: Fisica della Regola del 3x Diametro
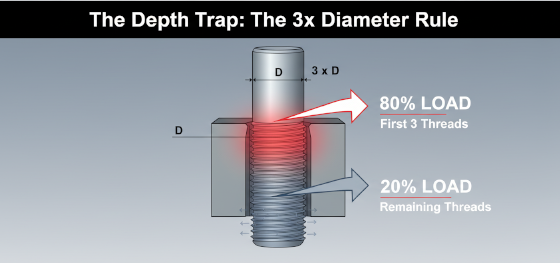
Uno dei miti più pericolosi nella progettazione meccanica è che una filettatura più lunga sia una filettatura più resistente. I progettisti spesso pensano che se una filettatura profonda 10 mm è buona, una profonda 20 mm deve essere due volte più sicura. La fisica non è d'accordo. In un assemblaggio standard di elementi di fissaggio, le prime tre filettature sopportano circa il 75% all"80% dell'intero carico. Quando si arriva alla sesta filettatura, la resistenza aggiuntiva diventa trascurabile. Questa è la base della "Regola del 3x Diametro" presente in ogni professionista Guida alla Progettazione di Filettature CNC. For a 5mm bolt (M5), a thread deeper than 15mm adds zero functional value while exponentially increasing the risk of tool failure.
The deeper a tap goes into a hole, the more friction it encounters. In materials like Acciaio Inossidabile o Titanio, this friction generates intense heat and makes chip evacuation nearly impossible. The spiral flutes of a tap have limited space; once that space is packed with compressed metal chips, the tap will seize and snap. JUCHENG’s rule of thumb is simple: aim for a thread depth of 1.5x to 2x the diameter for most applications. If you absolutely must have a deep thread, we suggest using a "Relieved Shank" design or switching to thread milling. By curbing the urge to over-design the depth, you allow us to maintain a faster, safer, and much more cost-effective production cycle. We don't want you to pay for deep holes that offer no mechanical advantage.
Interno vs. Esterno: Gestione di Classi di Accoppiamento e Tolleranze
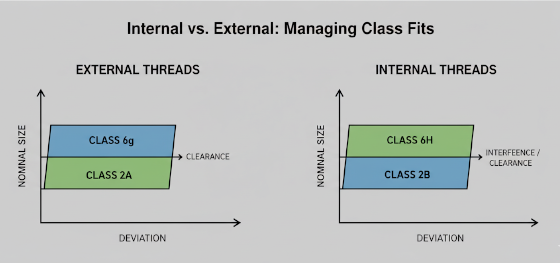
Threading is not a binary state—it is a spectrum of clearance and interference. In linee guida di progettazione per la lavorazione CNC, we refer to this as "Class of Fit." For internal threads (tapped holes), the standard is typically 6H or 2B. For external threads (bolts and shafts), it is 6g or 2A. These designations define the specific gap between the screw and the hole. If you design a part that will later be powder-coated or anodized, you must account for "Coating Growth." A standard anodize layer will add thickness to the tooth of the thread, making a "perfect" fit impossible to assemble.
At Jucheng Precision, we manage this through proactive tool-path offsets. If we know your aluminum part is destined for a heavy Type III Hardcoat, we will machine the internal threads to a 6G (over-sized) class. This allows the finish to grow into the dimensions required for a standard bolt. External threads on long shafts present another challenge: runout. If the thread is not perfectly concentric with the shaft's axis, the fastener will bind. We utilize single-point turning on our CNC lathes to ensure that external threads are cut in the same setup as the primary diameters. This technical alignment is the only way to guarantee a smooth, hand-tight fit in complex mechanical assemblies. We guide our clients through these tolerance choices to ensure that the final product doesn't require a tap-and-die "cleanup" after it leaves our factory.
L'Equazione del Foro per Maschio: Logica della Percentuale di Filettatura
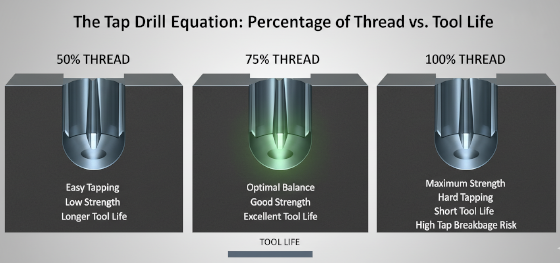
The strength of a thread is not determined by its sharpness, but by the "thread engagement percentage." Most engineers assume that a thread should be 100% full—meaning the internal and external teeth are perfectly interlocked. In reality, a 100% thread is a manufacturing disaster. It requires the tool to remove a massive amount of material from a tight space, leading to extreme torque and instant tool breakage. The industry standard we follow at Jucheng Precision is the "75% Rule." A thread that is 75% full provides over 95% of the strength of a 100% thread but requires only 40% of the cutting force.
This Guida alla Progettazione di Filettature CNC encourages the use of slightly larger pre-drill holes (tap drills). For an M6x1 thread, a standard 5.0mm drill provides roughly 77% engagement. In tough materials like Inconel, we might suggest a 5.1mm drill to reach a 65% engagement. This subtle shift reduces the load on the tap by half, significantly lowering the risk of part rejection. We provide our clients with optimized "Tap Drill Charts" during the DFM phase, ensuring that the hole you specify in your CAD matches the physical torque limits of the chosen material. By balancing engagement with manufacturability, JUCHENG delivers threads that are structurally invincible without the unnecessary risk of brittle tool failure.
Fresatura di Filettature: Lo Scudo Strategico per Leghe di Alto Valore
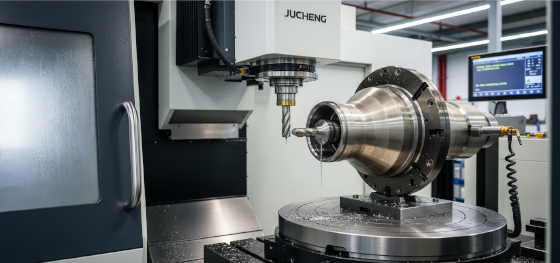
Tapping is a "one-and-done" process—fast, but binary. If the tap breaks, the part is often lost. For high-value aerospace components or medical manifolds made from PEEK, Jucheng Precision shifts the strategy to thread milling. A thread mill is a rotating tool that spirals its way down a hole to carve the thread profile. Because the tool is smaller than the hole diameter, it has massive advantages in chip evacuation and safety. If a thread mill breaks, it doesn't get stuck in the hole like a tap; it can simply be removed, a new tool inserted, and the operation resumed.
Thread milling also allows for total geometric freedom. We can use a single milling tool to create internal and external threads of any diameter, as long as they share the same pitch. It is the definitive solution for large-diameter holes where a standard tap would be physically too large to drive. More importantly, it allows us to control the thread fit down to the micron. If we find that a thread is a bit too tight during our in-process QC, we can simply adjust the tool offset and take a second "clean-up" pass. This level of iterative control is what allows JUCHENG to deliver perfect threads in materials that other shops find "un-tappable." We prioritize process security over raw speed because we know that for your most critical parts, a 100% yield rate is the only metric that matters.
Standard di Affidabilità di JUCHENG: Pianificazione del Processo per Filettature
At Jucheng Precision, we don't just "push buttons" on a machine. Threading is treated as an engineered sub-system of the processo di lavorazione CNC. Our reliability standard starts with tool selection—we only use premium cobalt-infused or vanadium-carbide taps designed for specific material groups. We don't use "general purpose" tools on your specialized parts. We also utilize high-pressure through-spindle cooling to physically blast chips out of blind holes, ensuring the tool never re-cuts waste material.
Our quality control department utilizes a "double-verification" method for all threaded features. We use physical Go/No-Go gauges for functional validation, and for high-precision components, we use optical comparators to verify the actual tooth profile and root radius. This ensures that your parts won't just "screw together," but will withstand the structural fatigue and vibration of the real world. Whether you are building an innovative heart pump or a mission-critical satellite mount, our expertise in thread engineering clarifies your design vision. We bridge the gap between a digital helix and a mechanical fit that lasts a lifetime. Contact Jucheng Precision today for a technical DFM review and see how our threading protocols can stabilize and elevate your next precision project.

