


Specifying premium chemical finishes on engineering blueprints frequently triggers catastrophic factory nightmares if the designer lacks true thermodynamic experience. Demanding a flawless aluminum anodized exterior seems incredibly simple until your tightest mechanical bearing press-fits violently seize during final assembly. Hardware procurement managers constantly hemorrhage venture capital funding because they blindly assume chemical surface treatments have zero physical impact on raw digital CAD dimensions.
Transforming raw extruded metal into a scratch-resistant masterpiece requires navigating highly aggressive sulfuric acid baths. Submerging pristine Lavorazione CNC components into electrified chemical vats physically alters the entire outer molecular structure of the billet. Failing to mathematically compensate for this aggressive chemical growth mathematically guarantees your expensive Aluminum chassis will completely fail strict quality control inspections upon arrival.
Surviving brutal marine environments heavily dictates pushing past standard cosmetic treatments entirely. Engineering maritime drone housings or heavy robotic joints practically requires deploying a military-grade Type III hardcoat to prevent immediate saltwater destruction. Executing this specific deep-penetrating process creates a massive dielectric oxide layer that actively resists extreme kinetic abrasion and horrifying chemical corrosion simultaneously.
Operating deep inside the Shenzhen precision manufacturing hub equips our veteran supply chain directors to actively block these devastating callout errors. We relentlessly force mechanical engineers to calculate exact dimensional tolerance stacking scenarios before the cutting spindle ever turns. Delivering truly functional hardware dictates that your primary machine shop must completely control the final chemical plating outcome without pointing fingers at third-party vendors.
contenuto:
Defeating Dimensional Tolerance Stacking
Mastering Type III Hardcoat Physics
Navigating Aerospace Alloy Color Variations
JUCHENG Hub: Dominating Surface Treatments
Frequently Asked Questions: Chemical Coatings
Defeating Dimensional Tolerance Stacking
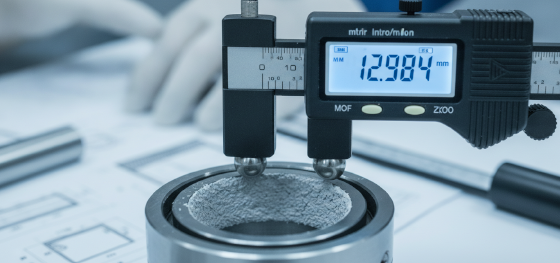
Does throwing a raw machined part into a chemical bath actually change its physical size?
Absolutely. The electrochemical oxidation process physically consumes microscopic layers of the base metal while simultaneously growing a brand new crystalline oxide structure outward, actively increasing the total geometric volume of the component.
Gestire l'accumulo spaventoso delle tolleranze dimensionali separa i programmi hardware d'élite dai progetti amatoriali. Gli ingegneri che progettano involucri pneumatici a tenuta stagna Pressofusione devono comprendere a fondo che un rivestimento chimico di cinquanta micron cresce di venticinque micron verso l'interno e spinge venticinque micron verso l'esterno. Non sovradimensionare matematicamente i fori filettati interni prima del bagno acido significa che i bulloni standard si strapperanno violentemente e si gripperanno all'istante durante l'assemblaggio.
Eseguire collegamenti meccanici impeccabili richiede rigorosamente protocolli estremi di mascheratura chimica sul piano di fabbrica. I tecnici d'élite utilizzano tappi in silicone altamente specializzati e ad alta temperatura per tappare meticolosamente ogni singolo foro di cuscinetto critico e filettatura a passo fine prima che il pezzo tocchi mai l'acido solforico. Proteggere queste geometrie nude garantisce che i press-fit dei cuscinetti rimangano completamente intatti dal rigonfiamento dimensionale.
Ridurre i colli di bottiglia dell'assemblaggio richiede un'intensa compensazione della programmazione CAM. I macchinisti intelligenti tagliano deliberatamente i perni esterni leggermente più piccoli e alesano i fori interni significativamente più grandi, anticipando specificamente l'inevitabile espansione geometrica. Affidarsi a una catena di fornitura frammentata dove l'officina meccanica non comunica mai con l'impianto di placcatura garantisce completamente disastrosi guasti da interferenza sulla tua linea di produzione.
Mastering Type III Hardcoat Physics

L'ossidazione cosmetica standard proteggerà un pesante collegamento robotico da gravi graffi cinetici?
Mai. Il processo standard di Tipo II fornisce semplicemente una pelle colorata microscopica e decorativa. Sopravvivere a un'abrasione fisica brutale richiede rigorosamente di spingere alte tensioni attraverso acido freddo gelido per costruire una barriera massiccia e impenetrabile simile allo zaffiro di Tipo III.
L'implementazione del rivestimento duro di Tipo III di grado militare trasforma completamente le capacità meccaniche fondamentali delle leghe grezze. La lavorazione di billette aerospaziali sotto questi parametri termodinamici estremi genera una superficie incredibilmente densa con livelli di durezza Rockwell che rivaleggiano con l'acciaio per utensili temperato. I team di approvvigionamento hardware specificano aggressivamente questo trattamento esatto per ingranaggi industriali massicci e piastre di usura scorrevoli per eliminare completamente il degrado da attrito.
Costruire uno spesso strato di ossido dielettrico fornisce profondi vantaggi di isolamento elettrico per dispositivi medici sensibili. Gli involucri metallici nudi conducono naturalmente spaventosi cortocircuiti elettrici che friggono all'istante le delicate schede madri interne. Applicare cinquanta micron di ossido cristallino denso blocca attivamente immense tensioni elettriche, agendo come uno scudo non conduttivo permanente e integrato che protegge i tuoi costosi circuiti.
Le limitazioni estetiche limitano pesantemente i progettisti che utilizzano rivestimenti duri pesanti. Poiché la struttura cristallina densa cresce così spessa, i pori metallici naturali si chiudono aggressivamente, rendendo praticamente impossibile assorbire coloranti liquidi brillanti e vivaci. Gli ingegneri devono accettare che i veri rivestimenti di grado militare si polimerizzano naturalmente in grigi scuri, bronzi o neri opachi utilitaristici.
| Metodo di lavorazione chimica | Spessore del rivestimento (micron) | Resistenza all'abrasione e all'usura | Applicazione Ottimale in Fabbrica |
|---|---|---|---|
| Tipo II Standard (Cosmetico) | 5 to 25 Microns | Low (Easily scratched by steel) | Premium colored consumer electronics |
| Type III Hardcoat (Mil-Spec) | 25 to 100 Microns | Extreme (Sapphire-like hardness) | Heavy robotic linkages and sliding gears |
| Chemical Conversion (Alodine) | Practically Zero | Zero (Acts only as a paint primer) | Internal electrical grounding chassis |
| Nichelatura chimica | 10 to 50 Microns | Very High (Smooth lubricity) | Valvole pneumatiche per fluidi ad alta pressione |
Navigating Aerospace Alloy Color Variations
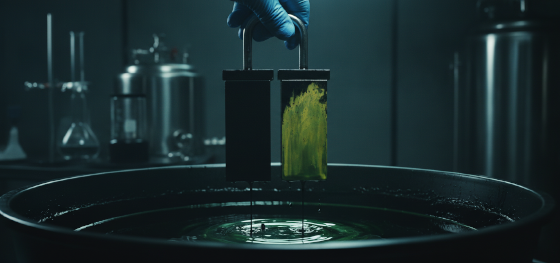
Can a factory guarantee that all different metal grades will absorb cosmetic black dye identically?
Absolutely not. The specific chemical elements alloyed inside the raw metal billet actively interfere with the dye absorption, causing massive, unpredictable color variations across different part numbers.
Designing complex assemblies containing multiple different aluminum anodized components introduces severe cosmetic risks. Machining a baseplate out of standard 6061 billet yields a flawless, deep mirror-black finish. However, milling the attached suspension arms out of ultra-strong 7075 aerospace billet chemically prevents the dye from penetrating perfectly. The heavy zinc content inside the 7075 structure forcibly turns the "black" dye into an ugly, mottled yellowish-green tint.
Protecting your premium retail aesthetics absolutely demands utilizing consistent raw material grades across your entire visible assembly. Hardware startups frequently make the terrifying mistake of machining a prototype out of solid billet, then switching to heavy Stampaggio a iniezione or die-cast alloys for mass production. Cast metals contain massive amounts of silicon, which chemically turns completely muddy and dark grey when exposed to standard oxidation baths.
Mitigating these visual disasters requires deep metallurgical authority before finalizing the purchase order. Veteran factory planners actively steer industrial designers away from impossible material combinations. When extreme 7075 yield strength is structurally mandatory, we strongly recommend deploying advanced secondary Verniciatura or powder coating to guarantee uniform external aesthetics.
JUCHENG Hub: Dominating Surface Treatments
Why do aggressive hardware startups refuse to bounce their raw machined parts to isolated chemical plating shops?
Because splitting the manufacturing liability completely destroys quality control. When the final coated part fails inspection, the machinist blames the plating thickness, and the plater blames the machinist's tolerances.
Partnering with Jucheng Precision entirely eliminates this toxic, disjointed supply chain friction. We aggressively calculate exact aluminum anodized dimensional growth models directly into our CAM milling programs. Executing the raw material cutting and the final chemical oxidation under one massive Shenzhen roof ensures absolute engineering accountability from start to finish.
Delivering flawlessly sealed medical and aerospace components dictates deploying uncompromising Design for Manufacturability (DFM) audits instantly. We actively identify impossible blind holes that will dangerously trap boiling caustic acids. Securing these physical vulnerabilities prevents terrifying downstream chemical bleeding that destroys your premium assemblies weeks after leaving our factory floor.
Frequently Asked Questions: Chemical Coatings
Will deep surface scratches immediately cause an oxidized aerospace bracket to red rust?
No. Non-ferrous alloys fundamentally cannot produce red iron-oxide rust. A deep mechanical scratch simply exposes the shiny raw silver metal beneath, which will naturally oxidize slightly against the ambient air but absolutely will not spread violently like rusting steel.
Does the intense chemical oxidation process successfully hide deep CNC tool marks?
Actually, it heavily magnifies them. Chemical conversion builds a perfectly uniform crystalline layer directly mirroring the underlying substrate topography. Any rough chatter marks, scratches, or jagged ridges left by a dull cutting spindle will become aggressively visible and shiny once the final sealing phase finishes.
Is it possible to chemically strip and re-coat a rejected enclosure without ruining it?
Yes, but it is incredibly destructive. Stripping the original oxide layer physically dissolves another microscopic layer of the base metal. Re-processing the same part practically guarantees your critical bearing dimensions will fall completely out of tolerance, rendering the salvaged component useless for precision assemblies.

